How to ensure dimensional accuracy in production is not a question answered by one final inspection. It begins with a controlled process, clear drawings, stable materials, and measurement methods that match the part’s function. A 0.02 mm deviation may appear minor on paper, yet it can prevent a bearing from seating or create vibration in an assembled unit. Temperature matters too. A steel component measured at 30°C may not match its inspection result at 20°C.
Lord Kelvin, a pioneer in scientific measurement, stated, “When you can measure what you are speaking about, and express it in numbers, you know something about it.” His principle remains practical on the shop floor. Engineers must define datums, verify calibration, and confirm whether micrometers, gauges, or coordinate measuring machines provide suitable resolution. A fixture should hold the part firmly without distorting it. Operators should also record tool wear, machine drift, and inspection conditions.
Small details matter.
Reliable production depends on more than accurate equipment. It requires repeatable methods, trained people, and evidence collected over time. Gauge R&R studies can reveal whether measurement variation is larger than the tolerance itself. Statistical process control can expose a gradual shift before rejected parts fill a bin. Still, no factory is perfectly stable. A clean inspection report may hide poor sampling or an overlooked burr. That uncomfortable possibility deserves attention. This guide explores practical ways to improve dimensional control, reduce avoidable variation, and build a process that remains dependable beyond a single successful batch.
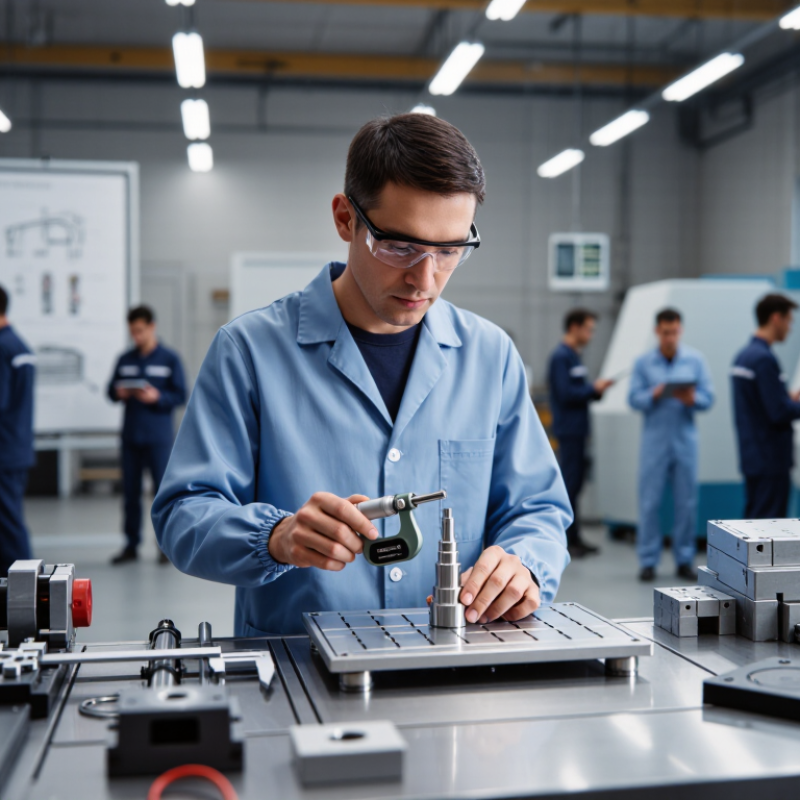
How to Ensure Dimensional Accuracy in Production
Dimensional accuracy is the degree to which a manufactured part matches its specified measurements. It describes the difference between the actual size and the size shown on the technical drawing. A shaft designed at 20.00 millimeters may measure 19.98 millimeters after machining. Whether that result is acceptable depends on the stated tolerance. Dimensional accuracy affects assembly, safety, performance, and product consistency. Without it, even a visually perfect component can fail during installation.
In production, accuracy begins with clear drawings and realistic tolerances. Operators should understand critical dimensions before machining starts. Calibrated measuring tools, such as micrometers and coordinate measuring equipment, help verify each feature. For example, checking a hole at several points can reveal taper or uneven cutting. That small detail often explains why parts fit differently. Temperature matters too. Metal can expand during inspection, creating misleading readings. Measuring at a stable temperature improves reliability.
Inspection records should connect measurements with machine settings, materials, and production times. This evidence helps teams identify repeated variation instead of guessing. However, measurement systems are not flawless. A dirty contact surface or hurried reading can distort results. This is where disciplined checking matters. A reliable process includes tool calibration, sample inspection, and corrective action when results drift. Perfect control is unrealistic. Reviewing mistakes honestly is more useful than hiding them, especially when a dimension repeatedly approaches its tolerance limit.
Dimensional accuracy describes how closely a manufactured part matches its specified nominal dimensions. The chart shows the mean absolute deviation from a 50.00 mm nominal dimension across common production stages. Lower deviation indicates greater accuracy; the 50 μm line represents the maximum acceptable deviation for this example.
Production insight: Monitoring dimensional deviation after machining, inspection, and final assembly helps identify process drift early, reduce rework, and maintain consistent fit and function.
How to Ensure Dimensional Accuracy in Production
Dimensional variation rarely comes from one machine alone. It may begin with material thickness, tool wear, thermal expansion, clamping force, or operator technique. On a production floor, a steel part can grow several micrometres during a warm afternoon. That change may appear small. It can still affect a tight fit.
NIST Technical Note 1297 states that measurement uncertainty must be evaluated with the result, not treated as an afterthought. This matters when a drawing tolerance is only 0.02 mm. If the measurement uncertainty approaches that limit, the inspection decision becomes weak. Industry Measurement Systems Analysis guidance commonly treats Gage R&R below 10% as acceptable, 10–30% as conditional, and above 30% as unacceptable. The numbers are useful, but not magical.
Trace variation back to its source. Record tool offsets, machine temperature, batch numbers, fixture changes, and inspection timing. Compare parts from the first, middle, and final production stages. A control chart can expose gradual tool wear, while a capability study can show whether variation is stable. ISO 14253-1 also warns against declaring conformity when measurement uncertainty overlaps the specification limit. That uncomfortable zone deserves review. Sometimes the process is blamed too quickly. Sometimes the gauge is trusted too easily. A loose fixture may leave witness marks on one edge, while a polished surface hides the same error elsewhere. Small details matter.
Dimensional accuracy begins with choosing the right measurement method, not the fastest one. Match each tool’s resolution and range to the drawing tolerance. A coarse instrument can hide small but costly deviations. For tight features, verify repeatability and measurement uncertainty before approving production parts. Calibration records should remain traceable to recognized national or international standards. Environmental control matters too. Temperature changes can alter metal dimensions during inspection. Keep parts and instruments in the same controlled area whenever possible.
Tips: Use a calibrated tool, clean the contact surfaces, and check the zero point before measuring. Measure from the specified datum, not from a convenient edge. Record the operator, instrument, temperature, and result. This detail supports reliable decisions later. Train inspectors with practical examples, because written procedures alone may not prevent mistakes.
I once treated repeated readings as proof of accuracy. They were consistent, but the reference surface was damaged. The process had repeated the same error perfectly. That experience changed our checks. We now compare critical tools against a certified reference and review unusual trends before releasing a batch. A suitable standard must fit the feature, tolerance, and risk. It should also be realistic for the shop floor. Overly complex controls can be ignored under pressure. A simple, documented method often performs better, though it still needs regular review.
Dimensional accuracy depends on more than a precise cutting tool. Every machining process needs controlled inspection and dependable calibration. In production work, I have seen a small temperature change affect readings on a tight-tolerance shaft. The inspection area should remain stable, clean, and free from unnecessary vibration. Parts must cool before measurement. Measuring a warm component can create false confidence.
Use calibrated micrometers, gauges, and coordinate measuring equipment for critical features. Verify zero settings before each shift. Check reference standards at planned intervals. Calibration records should show the equipment ID, date, technician, reference standard, and measurement uncertainty. This information supports traceability and helps auditors trust the results. It also reveals repeated drift.
Inspection frequency should match process risk. A high-volume bore may need first-piece, in-process, and final checks. Record actual values, not only pass or fail decisions. A 20.000 mm bore measuring 20.018 mm shows more useful information than a simple approval mark. Trend these results to identify tool wear before parts fall outside tolerance. Small changes matter.
Yet no plan is perfect. A checklist can still miss an operator’s measuring pressure or a dirty contact surface. I once treated stable readings as proof of a stable process. That assumption needed review. Cross-check unusual results with another calibrated instrument, then inspect the fixture, method, and environment. Reliable control comes from questioning measurements, not merely collecting them.
How to Ensure Dimensional Accuracy in Production
Dimensional accuracy improves when teams analyze results, not just collect them. Start with traceable measurements from calipers, CMMs, and optical systems. Record operator, machine, material batch, temperature, and tool condition. These details expose hidden variation. A control chart can show whether drift began after a tool change. Review Cp and Cpk values by product family, not only by monthly averages. One average can hide a serious shift.
Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturing leaders expect smart operations to become a primary competitiveness factor within five years. That expectation requires usable data, not attractive dashboards. Separate repeatability from reproducibility through a gauge R&R study. If different operators obtain different readings, process adjustments may be misleading. We learned this the hard way. Our first dashboard reported stable output, but it excluded rejected parts.
Use weekly Pareto reviews to rank dimensional defects by frequency and cost. Then test one corrective action at a time. Adjust cutting speed, fixture pressure, or inspection intervals only after establishing a baseline. NIST guidance on measurement system evaluation stresses uncertainty and traceability during reliable decision-making. Keep calibration records beside production results. Recheck the process after maintenance, material changes, or extended downtime. Small deviations matter. A 0.08-millimeter shift may become a recurring customer complaint when tolerance margins are narrow. Feedback must reach operators quickly, while the evidence remains clear.
| Feature Characteristic | Nominal Dimension | Tolerance | Lower Specification Limit | Upper Specification Limit | Average Measurement | Standard Deviation | Cpk | Out-of-Specification Rate | First-Pass Yield | Process Status |
|---|---|---|---|---|---|---|---|---|---|---|
| Shaft Diameter | 25.00 mm | ±0.03 mm | 24.97 mm | 25.03 mm | 25.004 mm | 0.008 mm | 1.08 | 1.2% | 98.1% | Monitor variation |
| Bore Diameter | 20.00 mm | ±0.04 mm | 19.96 mm | 20.04 mm | 20.001 mm | 0.006 mm | 2.17 | 0.1% | 99.7% | Stable |
| Overall Length | 120.00 mm | ±0.10 mm | 119.90 mm | 120.10 mm | 119.995 mm | 0.022 mm | 1.59 | 0.4% | 99.2% | Capable |
| Hole Center Position | 50.00 mm | ±0.05 mm | 49.95 mm | 50.05 mm | 50.008 mm | 0.012 mm | 1.17 | 0.9% | 98.8% | Check fixture alignment |
| Wall Thickness | 3.00 mm | ±0.05 mm | 2.95 mm | 3.05 mm | 3.002 mm | 0.010 mm | 1.60 | 0.3% | 99.4% | Capable |
| Flatness | 0.00 mm | ≤0.08 mm | 0.00 mm | 0.08 mm | 0.031 mm | 0.014 mm | 1.17 | 0.8% | 98.9% | Review clamping method |
| Analysis and improvement actions: Prioritize shaft diameter and hole center position because their Cpk values are below 1.33. Verify tool wear, fixture alignment, temperature stability, and measurement-system calibration. Continue statistical process control using control charts and review capability after corrective actions. Cpk is calculated using the specification limits, process average, and standard deviation; a Cpk of 1.33 or higher is commonly used as a capable-process target. | ||||||||||
Material thickness, tool wear, heat, clamping force, and operator technique can all change dimensions. A warm steel part may grow several micrometres. Small changes can affect a tight fit.
Record tool offsets, machine temperature, batch numbers, fixture changes, and inspection timing. Compare parts from early, middle, and late production. Control charts can reveal gradual tool wear.
Metal can expand during a warm inspection period. Let parts cool before measuring them. Keep parts and instruments in the same controlled area. Temperature control is not optional for tight tolerances.
Match the tool’s range and resolution to the drawing tolerance. A coarse instrument may hide a costly deviation. Verify repeatability and uncertainty for critical features. Faster is not always better.
Use a calibrated tool. Clean contact surfaces. Check the zero point before measuring. Measure from the specified datum, not a convenient edge. Record the operator, temperature, instrument, and result.
Records show the equipment identification, date, technician, reference standard, and uncertainty. They support traceability and reveal repeated measurement drift. Paperwork alone cannot fix a poor method.
Inspection frequency should match process risk. A high-volume bore may need first-piece, in-process, and final checks. Record actual values, such as 20.018 mm, not only pass or fail.
Repeat the check with another calibrated instrument. Inspect the fixture, contact surfaces, method, and environment. A damaged reference can produce perfectly consistent errors. Our earlier assumption was wrong.
Dimensional accuracy is the ability of a manufactured part to match its specified measurements within an acceptable tolerance. It plays a critical role in product performance, assembly, safety, and consistency. To understand how to ensure dimensional accuracy in production, manufacturers must first identify possible sources of variation, including machine wear, tool deflection, thermal changes, material behavior, operator practices, and unstable process conditions.
Reliable measurement tools and clearly defined standards provide the foundation for accurate inspection. Production teams should select instruments appropriate to the required tolerance, maintain them properly, and calibrate them at planned intervals. Machining processes can then be controlled through in-process checks, first-piece inspections, and final verification. By recording and analyzing measurement results, teams can recognize trends, locate recurring causes, and adjust machine settings, tooling, or work methods. Continuous review and corrective action help reduce variation, improve process stability, and maintain consistent dimensional quality over time.
Singer Cast