In 2026, mold performance depends on more than achieving a clean first shot. Designers must balance cycle time, part quality, tool life, energy use, and production consistency. Grand View Research estimated the global injection-molded plastics market at USD 284.6 billion in 2024, with projected growth through 2030. That scale raises the cost of preventable defects. A warped panel or a poorly cooled rib can turn a promising design into hours of rework.
The practical question is how to optimize mold design for better performance without relying on simulation alone. This guide examines gate placement, cooling-channel layout, venting, material selection, and maintenance access. It connects each choice to measurable outcomes, such as fill balance, cooling time, scrap rate, and dimensional stability. Deloitte and the Manufacturing Institute projected that U.S. manufacturing could need 3.8 million workers by 2033, with 1.9 million jobs potentially unfilled. That workforce pressure makes repeatable, easier-to-run tooling especially valuable. Still, a polished simulation can miss a stubborn real-world short shot. Resin variation, machine settings, and operator feedback matter. The recommendations ahead combine engineering checks with shop-floor observations, while recognizing that every mold has limits.
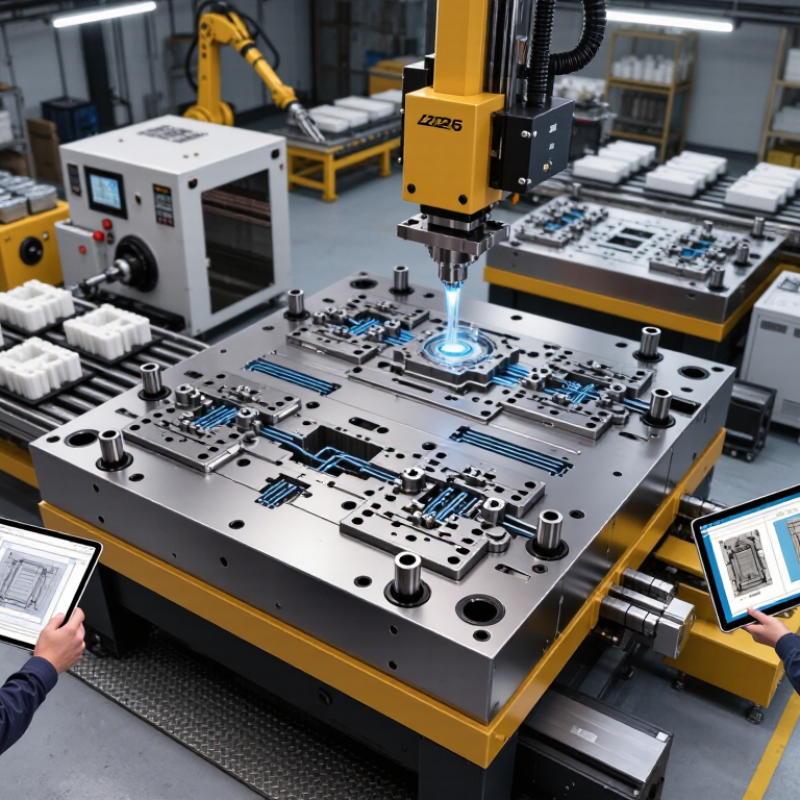
Set measurable targets before drawing the mold: cycle time, scrap rate, cavity-to-cavity weight variation, tool life, and maintenance access. A faster nominal cycle is not a gain if warped parts require sorting. Small details matter. Cooling-channel layout, gate position, venting, resin shrinkage, and machine capacity all constrain what the tool can deliver. A design that ignores clamp force or shot capacity may look sound in CAD and still fail on the press.
PlasticsEurope’s 2024 Fast Facts report estimates global plastics production at 413.8 million tonnes in 2023. That scale makes small per-part losses consequential, but the figure does not prove that any single mold change will reduce scrap. Deloitte’s 2024 Smart Manufacturing survey found that 86% of respondents expect smart manufacturing to drive competitiveness within five years. For mold design, that supports planning for useful process data, not adding sensors without a clear decision to inform. One easy-to-miss risk is trusting simulation inputs too much. Resin data and boundary conditions are not perfect. Compare predictions with trial measurements, then adjust cooling or venting where the part actually shows uneven shrinkage or trapped air.
Material choice should follow the resin, expected output, and maintenance plan—not just purchase price. Glass-filled resins can abrade mold surfaces faster, while corrosive additives may call for more resistant tooling. Harder steel can last longer, but it may cost more to machine and repair. For short runs, aluminum may be practical when pressure, temperature, and wear remain within limits. Check compatibility with the actual resin early.
Mold geometry affects filling, cooling, and part removal. Keep wall thickness as uniform as the part allows; abrupt changes can create sink marks or uneven cooling. Add draft to vertical faces so parts release without scraping, and use generous radii at internal corners to reduce stress and improve flow. Place gates where flow paths can fill evenly, then add vents near likely air traps. Small details matter.
Cooling channels should follow the shape where practical, while leaving enough material around them for strength. A simulation can reveal hot spots, but it cannot replace a trial shot. Measure actual cycle time, dimensions, and surface defects, then adjust one feature at a time. The first layout may still be wrong. That is useful evidence, not a failure.
Arrange cavities to match the part family, not just to fit the steel. Keep runner branches similar in length and diameter, and place gates where melt can reach thin ribs before thick bosses freeze. Balanced flow reduces pressure differences and uneven packing. It is not perfect: complex parts may still need simulation and trial shots.
The Injection Molding Handbook, 3rd edition, identifies cooling as the dominant share of molding cycle time; practical benchmarks often put it near 70–80%, depending on the part and resin. So leave room for cooling channels close to heat-heavy areas, while avoiding channels that weaken the mold. Vent the last-fill regions, especially rib ends and corners. Poor venting can trap air, causing burns, short shots, or extra pressure. Use resin-specific vent-depth guidance; a universal setting can be wrong.
Tips: Map likely air traps before machining. Check first-shot fill patterns and burn marks, then adjust vents or gates in small steps. A tidy layout helps, but the first simulation can still miss real process variation.
| Design Area | Recommended Target or Check | Practical Design Action | How to Verify |
|---|---|---|---|
| Cavity layout and balance | Aim for cavity-to-cavity fill-time variation within approximately 5% of the average in a naturally balanced multi-cavity mold. | Use a symmetric layout and keep runner paths, cross-sections, and gate conditions as consistent as practical. | Compare cavity pressure traces and fill times during mold trials; confirm with a short-shot study. |
| Runner and flow path | Keep flow-path lengths and restrictions as uniform as possible from the sprue to each cavity. | Review runner turns, diameter transitions, and gate locations together. Avoid unnecessary sharp changes in section. | Use mold-flow analysis to identify pressure loss, unequal filling, and likely hesitation before cutting steel. |
| Gate placement | Place gates to promote a controlled fill pattern and reduce long, unbalanced flow paths. | Consider part geometry, wall thickness, weld-line locations, appearance, and gate vestige requirements when selecting gate type and position. | Check predicted weld lines and air traps in simulation, then inspect actual fill patterns and part quality. |
| Venting at the parting line | For many unfilled thermoplastics, an initial vent-depth range around 0.02–0.04 mm may be considered; the correct value depends on the resin and process. | Place vents at end-of-fill regions, weld-line locations, and other areas where air is likely to become trapped. Follow resin supplier and moldmaker guidance. | Look for burn marks, incomplete filling, and trapped-air evidence. Confirm vent dimensions against the material’s processing requirements. |
| Vent land and relief | A vent land of roughly 3–6 mm is a common starting point for design review, subject to part geometry and material behavior. | Provide a downstream relief path so displaced air can escape without creating excessive flash risk. | Inspect vent areas after trials for blockage, wear, flash, or signs that the vent path is insufficient. |
| Process validation | Establish a stable process window for fill, pack, and cooling rather than relying on a single successful shot. | Record cavity-specific pressure and temperature data where available, and document changes to gates, runners, or vents. | Run repeatable trials and compare part dimensions, weight, surface quality, and cavity-to-cavity consistency. |
How to Optimize Mold Design for Better Performance in 2026
Cooling often sets the pace of an injection-molding cycle. Society of Plastics Engineers technical guidance places cooling at roughly 70–80% of cycle time in many applications. Treat that as a starting benchmark, not a promise: wall thickness, resin, and mold temperature can shift the result. I would not trust the percentage blindly.
Design channels to follow the part’s shape and keep them close to thick sections, where heat lingers. Check flow balance, too. A cold spot near a rib can leave sink marks even when the average cycle looks efficient. Conformal channels may improve temperature uniformity, but their cost and cleaning needs deserve scrutiny. Better on paper is not always better on the press.
Track inlet and outlet water temperatures, flow rate, part weight, and cycle time during trials. Change one variable at a time, then inspect several consecutive parts for warpage and surface defects. Small gains matter. Yet a faster cycle that creates rejects is not an improvement.
How to Optimize Mold Design for Better Performance in 2026
Validating Designs Through Simulation and Testing
A mold can look flawless on screen and still produce short shots, sink marks, or uneven cooling. Simulation helps reveal these risks before steel is cut. Engineers can study resin flow, pressure, temperature, and cooling time across the cavity. Pay close attention to thin ribs and sharp transitions; these areas often expose filling problems first. Small details matter.
Simulation is a guide, not proof. Check material data and process settings against the resin supplier’s specifications and the intended machine. Then compare predictions with trial runs, measuring part dimensions, weight, and visible defects. A temperature probe near a thick section may reveal a hot spot that the model missed. Record changes between runs, including gate adjustments and cooling time, so results stay traceable.
Not every mismatch has a simple fix. A model may assume ideal venting, while a real mold traps air at a parting line. That gap deserves investigation, not a quick design patch. Test parts under repeatable conditions, and involve tooling, process, and quality teams when results disagree. Leave room for another iteration. The first trial can teach more than a polished simulation.
Match the material to the resin, production volume, and maintenance plan. Glass-filled resin can wear mold surfaces faster. Short runs may suit aluminum when pressure, heat, and wear remain manageable. Purchase price alone can mislead.
Keep wall thickness as even as the part allows. Add draft to vertical faces and generous radii at internal corners. These details can reduce scraping, stress, and uneven cooling. Small changes matter.
Arrange cavities for the part family, not simply to fit the mold. Similar runner lengths and diameters can balance flow. Place gates so thin ribs fill before thick sections freeze. It may still take adjustment.
Put channels near heat-heavy areas where practical, while leaving enough material for mold strength. Thick sections can hide hot spots. Cooling often takes much of the cycle, but actual time varies.
Check last-fill areas, such as rib ends and corners. Trapped air may cause burns, short shots, or extra pressure. Use resin-specific vent guidance; one setting does not fit every mold.
Simulation can estimate flow, pressure, temperature, and cooling time. Pay close attention to thin ribs and sharp transitions. It is a guide, not proof.
Run trial shots under repeatable conditions. Measure dimensions and part weight, then inspect for sink marks, burns, and short shots. A probe near a thick section may uncover heat the model missed.
Record each change, including gate adjustments and cooling time. Check whether trapped air or process variation explains the mismatch. The first layout can be wrong. That is useful evidence, though it can be frustrating.
This article explains how to optimize mold design for better performance by connecting design decisions to clear production goals, such as part quality, consistency, and efficient cycle times. It covers how to account for manufacturing constraints, choose suitable materials, and define mold geometry that supports reliable operation. Careful attention to cavity layout, material flow, and venting can help reduce defects and promote uniform filling, while an effective cooling system helps manage temperature and shorten production cycles.
The article also highlights the value of validating a design before full-scale production. Simulation can reveal potential flow, cooling, or structural issues early, allowing designers to refine the mold with less trial and error. Testing then confirms whether the design performs as intended under practical conditions. Together, these steps provide a systematic approach to creating molds that are dependable, efficient, and suited to their production requirements.
Singer Cast